Standardizing the Fastener Procurement Process: From Requirements Definition to Mass-Production Review

Daniel
With experience in fastener manufacturing and export sales, we specialize in bolts, nuts, screws, self-drilling screws, fully threaded rods, and customized fastening solutions for construction, machinery, automotive, and industrial applications.
Introduction: Why Fastener Procurement Needs Process Standardization
In the daily procurement of manufacturing enterprises, screws, nuts, and other fasteners are often regarded as "small parts," but it is precisely these small parts that are most prone to information gaps in the inquiry, sampling, and mass production stages. Incomplete specification descriptions, inconsistent quotation bases, and samples that do not match mass-produced products are typical problems almost every procurement officer has encountered. A single misreading of a thread specification or an omission of a surface treatment item can lead to repeated communication, delivery delays, and even quality disputes.
Incorporating inquiry, supplier evaluation, sample verification, order production, and acceptance into a unified process can significantly improve cross-departmental collaboration efficiency and reduce procurement risks. The engineering department provides accurate technical conditions, the procurement department unifies commercial terms, the quality department establishes upfront inspection checkpoints, and the production department feeds back actual assembly performance—only when all these links use the same set of documents, the same version of drawings, and the same acceptance standards can fastener procurement truly be brought under control.
This article organizes management methods in the order of project progression, from requirement definition to mass production review, to help procurement, engineering, quality, and production teams establish an executable standard operating procedure.
I. Requirement Definition: First Make the Procurement Technical Conditions Clear
The first step in process standardization is not finding suppliers, but writing the requirements clearly. It is recommended to establish a unified requirements checklist covering at least the following elements: product name, application, drawing or applicable standard, specifications and dimensions, material, strength grade, surface treatment, quantity, delivery date, and packaging requirements. The more complete the checklist, the stronger the comparability of subsequent inquiries and price comparisons.
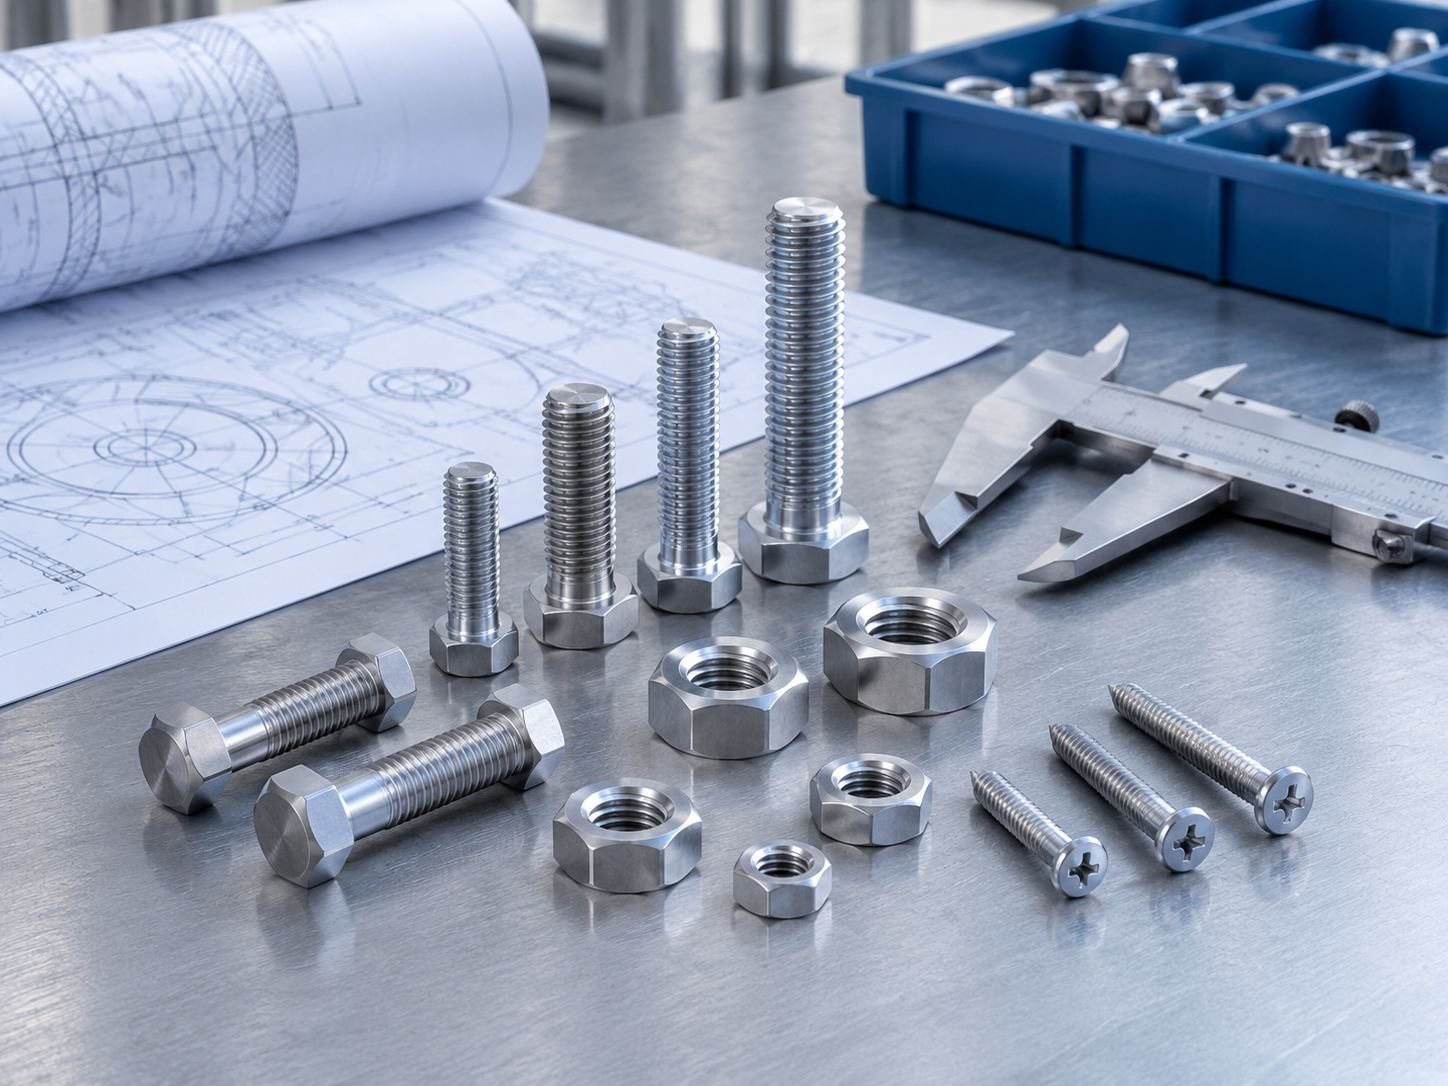
For products such as bolts, nuts, and studs, key dimensions and mating relationships must be clearly specified. When categories such as hex bolts and flange bolts are involved, the applicable standards and key tolerances should be marked to avoid situations where "the head type is correct but the thread precision does not match." For machine screw products, the drive recess type and head form must also be specified; for example, cross-recess countersunk head and slotted countersunk head differ significantly in assembly scenarios, and the selection should be stated directly in the requirements document.
Take cross-recess countersunk head machine screws DIN 965 as an example. This type of product belongs to metric thread fasteners and is suitable for scenarios such as electrical equipment, furniture, and panel assembly. The countersunk design allows the head to be flush with the mounting surface after fastening; the similar slotted countersunk head machine screw DIN 963 uses a straight-slot drive and countersunk head structure, commonly found in equipment panels, furniture hardware, and general assembly applications. Both can be supplied in steel, stainless steel, and brass versions. During procurement, the material, drive type, and standard number should be clearly specified in the requirements checklist rather than merely writing "countersunk screws."
At the same time, a distinction must be made between standard parts, non-standard parts, and special-shaped parts. For products with special requirements such as stainless steel fasteners and hot-dip galvanized bolts, the material grade, process route, and inspection basis should be stated. Finally, establish a requirement change record mechanism to ensure that engineering, procurement, and suppliers always use the same version of drawings and technical documents, with every modification leaving a trace.
II. Inquiry and Price Comparison: Making Quotations Comparable
The most common inefficiency in the inquiry stage is that each supplier quotes according to its own habits, making prices impossible to compare horizontally. The solution is to send a unified inquiry template to candidate fastener suppliers, requiring item-by-item quotations by specification, material, surface treatment, quantity, tooling cost, packaging, delivery date, and trade terms, with missing items deemed invalid quotations.
At the same time, confirm the quotation boundaries: whether tax, freight, testing fees, and special packaging fees are included, and specify the quotation validity period and raw material price adjustment mechanism. Fastener costs are highly correlated with steel prices, and quotations lacking price adjustment clauses are prone to disputes in long-cycle orders.
When comparing prices, compare total procurement cost rather than unit price, comprehensively considering quality risk, delivery stability, inventory capability, and after-sales response. A fastener manufacturer with a slightly higher unit price but good batch consistency is often more cost-effective than a supplier with a low price but frequent rework.
For cross-border procurement such as export of inch-standard bolts, it is also necessary to further confirm the standard version, document requirements, labels, packaging, and export delivery conditions. In this case, priority should be given to fastener export suppliers with export experience, and the division of responsibilities for shipping marks, packing lists, and certificates of origin should be clarified at the inquiry stage.
III. Supplier Admission: From Qualification Review to Capability Assessment
Supplier admission is not a one-time document collection but the establishment of a capability profile by category. First, verify the basic qualifications, production scope, quality management process, equipment, and testing capabilities of the fastener manufacturer or fastener supplier, and confirm that the business license scope is consistent with the actual production content.
Second, assess the match by category and process. When screening hex bolt manufacturers, flange bolt suppliers, or heavy hex nut manufacturers, focus on verifying actual manufacturing experience with the relevant products rather than merely looking at corporate promotional materials; for segmented suppliers such as self-tapping screw manufacturers and self-drilling screw suppliers, verify forming, heat treatment, surface treatment, and batch traceability capabilities. Carbon steel nut factories and stainless steel fastener manufacturers differ considerably in process, and the same set of standards should not be simply applied to both.
It is recommended to establish a supplier scoring table covering six dimensions: quality, cost, delivery, service, compliance, and continuous improvement, and to set audit frequency according to risk level. For high-risk categories such as high-strength bolts and hot-dip galvanized bolts, the proportion of on-site audits should be increased; for conventional standard parts, it can be appropriately simplified, concentrating management resources on key suppliers.
IV. Sample and Technical Confirmation: Moving Mass Production Risks Upstream
The sample stage is the lowest-cost window for controlling mass production risks. Before sample confirmation, the inspection plan should be clearly defined, including dimensions, threads, mechanical properties, material, surface treatment, and assembly fit, and the sampling quantity and acceptance rules should be agreed upon.
For custom socket head cap screw projects, custom special-shaped fastener projects, and non-standard fastener machining projects, it is especially important to confirm the consistency among the four: drawings, samples, inspection standards, and approval records. The risk of custom parts often lies not in single-piece dimensions but in process stability during batch machining; therefore, sample review should invite engineering and production assembly personnel to participate jointly.
Suppliers should be required to provide material certificates, inspection reports, or necessary third-party verification documents, and the handling of nonconforming products should be defined in advance, including rework, remanufacture, and cost bearing. After sample approval, freeze the technical documents and limit samples; without written confirmation, materials, processes, or key dimensions must not be changed without authorization—this is the basis for subsequent change control.
V. Contracts and Orders: Putting Technical and Commercial Requirements into Documents
The order is the final carrier of technical and commercial requirements. Orders should be linked to approved drawings, technical specifications, sample records, and version numbers, avoiding placing orders based solely on verbal descriptions or chat records. In practice, a considerable proportion of fastener procurement disputes stem from "the order was not written clearly."
The contract should clearly specify quantity and delivery batches, delivery date, acceptance standards, packaging identification, traceability requirements, change control, and breach handling clauses. For in-depth cooperation such as fastener OEM manufacturing and custom bolt wholesale, supplementary requirements for tooling ownership, confidentiality obligations, intellectual property, and spare parts management should be added to prevent tooling disputes after the cooperation ends.
It is recommended to set an order confirmation checkpoint: the order takes effect only after the supplier signs back to confirm the key clauses, ensuring that procurement, engineering, quality, and the supplier have a fully consistent understanding of technical requirements, delivery dates, and acceptance methods.
VI. Production Follow-up and Change Control: Ensuring Consistency Between Samples and Mass Production
After the order is placed, track the status of raw material arrival, production scheduling, key processes, surface treatment, and finished product inspection by milestone, and identify delivery risks in advance. For delivery-sensitive orders, suppliers may be required to provide weekly progress feedback.
Suppliers are obliged to proactively report anomalies affecting quality or delivery, while the buyer should record the cause, corrective actions, responsible persons, and completion time to form a traceable anomaly ledger. Any change in material, process, equipment, site, or subcontracting should first be assessed for impact and obtain written approval—this is the core mechanism for ensuring "consistency between samples and mass production."
For high-risk suppliers such as high-strength bolt manufacturers and hot-dip galvanized bolt suppliers, first-article confirmation, process audits, or on-site inspection can be added. First-article confirmation should cover key dimensions and performance items, while process audits focus on the stability of heat treatment and coating process parameters.
VII. Incoming Inspection and Quality Closed Loop: From Inspection to Corrective and Preventive Action
Incoming inspection should establish sampling and acceptance plans based on procurement specifications, verifying quantity, appearance, dimensions, markings, material documents, and batch information. Inspection records should correspond one-to-one with order numbers and supplier batches to facilitate subsequent traceability.
Different product categories should have corresponding verification items set according to use. For example, expansion bolt wholesale products should focus on expansion sleeve fit and load-bearing performance, while products provided by lock nut suppliers need to have anti-loosening performance verified; countersunk machine screw products should focus on checking head angle and countersink fit to ensure the head is flush with the panel after assembly. When nonconformities are found, they should be isolated promptly and a review initiated to clarify the return, rework, concession acceptance, or replenishment process, preventing nonconforming products from entering the production line.
The key to a quality closed loop lies in data. Continuously evaluate supplier performance through nonconformity rate, on-time delivery rate, customer complaint rate, and corrective action closure rate, and feed the results back into the next round of admission assessment and order allocation, forming a true closed-loop management.
VIII. Mass Production Review and Continuous Optimization: Establishing a Replicable Procurement Mechanism
After the first mass production batch is completed, a review should be organized to compare quotations, actual delivery, quality performance, and production use feedback, identifying weak links in the process. Review conclusions should be translated into document updates rather than remaining only in meeting minutes.
On this basis, establish a preferred catalog of standard parts and a list of qualified suppliers, promote the normalization of specifications for screws, nuts, and commonly used fasteners, and reduce unnecessary customization and duplicate development. For multi-source categories such as machine screw wholesale and carriage bolt factories, alternative supply and safety stock strategies should be evaluated to reduce the risk of supply interruption from a single source.
Finally, through unified templates, digital order ledgers, and problem closed-loop records, achieve a procurement process that is traceable, auditable, and continuously improvable. The value of templates and ledgers lies in turning individual experience into organizational capability, so that personnel changes do not affect process stability.
Conclusion: Standardization to Connect the Entire Chain from Inquiry to Mass Production
The core of fastener procurement standardization is to implement demand, technical, commercial, quality, and delivery requirements into the same set of documents and node management. The process itself is not complex; what is difficult is for departments to consistently use the same version, the same standard, and the same recording method.
Enterprises can start with pilot programs on high-frequency procurement categories and key suppliers, then gradually expand to custom parts, export parts, and OEM projects. This article does not cite unverified industry statistics or case data; actual benefits should be evaluated in light of the enterprise's own procurement cycle, quality costs, and delivery performance.

